The global pursuit of sustainable and biocompatible materials has brought eucalyptus cellulose into the spotlight, particularly within the pharmaceutical and food industries. As a versatile plant-derived polymer, it provides a foundation for creating high-performance excipients that ensure stability and efficacy in various commercial applications. Understanding its structural properties is key to optimizing product quality in modern manufacturing.
From a technical standpoint, the processing of these plant fibers into microcrystalline forms allows for unprecedented control over tablet compressibility and drug release profiles. The industry is shifting toward high-purity derivatives that meet stringent pharmacopoeia standards, reducing reliance on synthetic alternatives while enhancing the safety profile of consumer products.
By leveraging the natural advantages of eucalyptus cellulose, manufacturers can achieve a perfect balance between mechanical strength and rapid disintegration. This synergy is essential for developing advanced delivery systems that improve patient compliance and product shelf-life across global markets.
The Chemical Essence of Eucalyptus Cellulose
At its core, eucalyptus cellulose serves as the biological precursor to Microcrystalline Cellulose (MCC), a white, odorless crystalline powder known for its exceptional compressibility. By refining the natural plant fibers, we obtain a material that is insoluble in water, ethanol, and organic solvents, making it an ideal inert carrier for active ingredients.
The molecular structure of this derivative is characterized by a high degree of crystallinity, which allows it to form stable gel structures. This unique architecture ensures that the resulting products possess high water absorption and expansion capabilities, which are critical for the disintegration of pharmaceutical tablets.
Industrial Production and Refining Processes
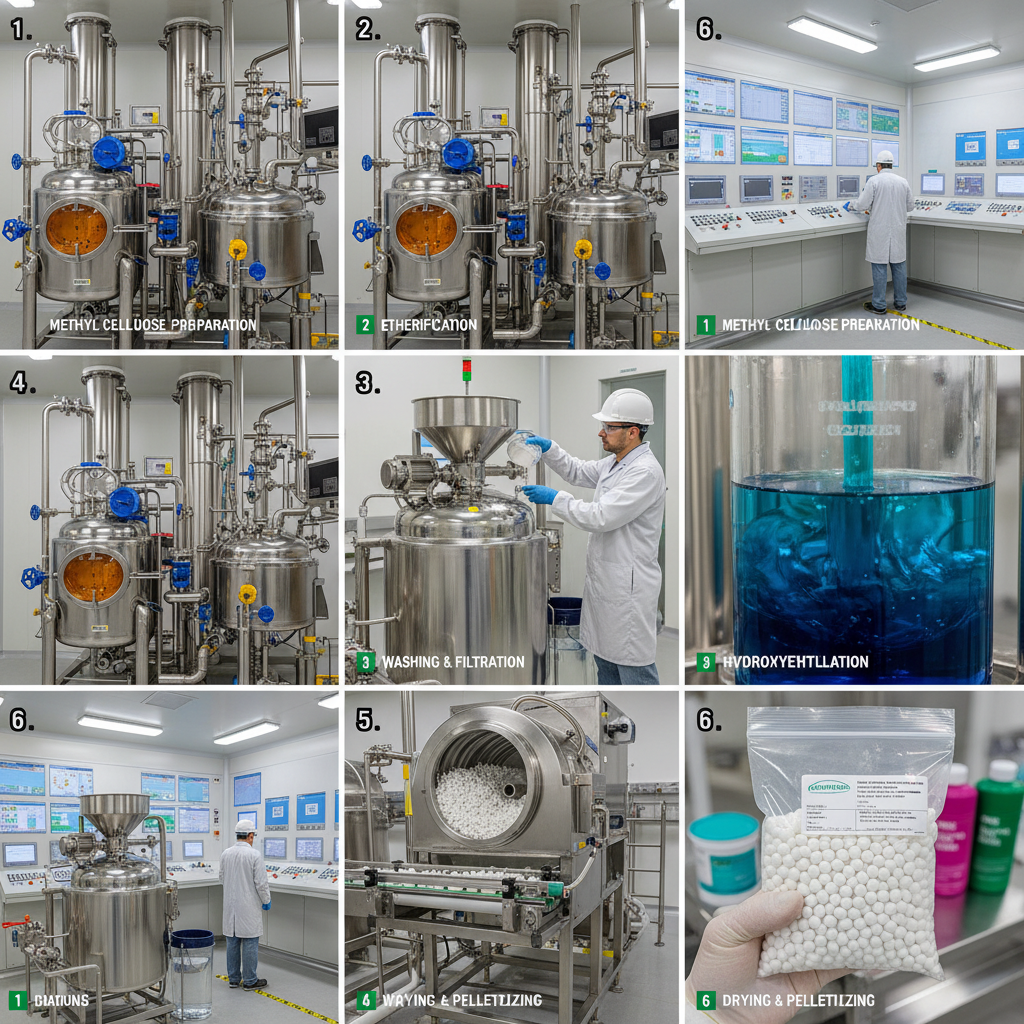
The journey from raw plant material to high-purity pharmaceutical grade begins with rigorous pretreatment. Natural sources, including vegetable pulp and specialized fibers, are processed to extract pure cellulose, ensuring that all impurities are removed before the chemical transformation begins.
One of the most prevalent methods is acid hydrolysis, where the β-1,4 glycosidic bonds are cleaved under acidic conditions. By removing the amorphous regions of the cellulose molecule, the material is degraded to a specific limit of polymerization (typically 15 to 375), resulting in the creation of microcrystalline cellulose with superior thermal stability.
Innovation has also introduced enzymatic hydrolysis and mechanical grinding as alternative pathways. The enzymatic approach is particularly valued for being a "green" process, utilizing cellulase to break molecular chains with significantly fewer chemical reagents, thereby reducing the environmental footprint of production.
Core Physicochemical Properties and Stability
The technical utility of eucalyptus cellulose stems from its non-ionic nature and chemical inertness. It remains stable across a wide pH range, which is vital when formulating drugs that might be sensitive to pH fluctuations during storage or digestion.
When processed into MCC, the material exhibits a highly porous particle structure. This porosity allows for a large drug-holding capacity, meaning that eucalyptus cellulose can effectively support active pharmaceutical ingredients (APIs) while maintaining a manageable tablet size.
Furthermore, its inability to dissolve in most organic solvents and oils prevents unwanted interactions in complex mixtures. This stability ensures that the physical integrity of the final product is maintained, regardless of the surrounding chemical environment.
Performance Analysis in Tablet Manufacturing
In tablet production, this material acts as a multi-functional agent, serving as a filler, binder, and disintegrant simultaneously. Its excellent fluidity allows for a homogeneous mix with other excipients, while its dry adhesion properties enable the creation of very hard tablets that do not crumble during transport.
By adjusting the dosage—typically between 5% and 30% depending on whether the process is wet granulation or dry compression—manufacturers can precisely control the dissolution rate of the medication, ensuring the drug is released in the body at the intended speed.
Comparative Performance of Cellulose Derivatives
Diversified Applications in Food and Cosmetics
Beyond pharmacy, eucalyptus cellulose derivatives are indispensable as anti-caking agents and stabilizers in the food industry. They prevent powdered foods from clumping and improve the overall texture and viscosity, ensuring that food structures remain stable and appealing to the consumer.
In the realm of skin care, these materials function as thickening agents. By increasing the viscosity of creams and lotions, they improve the spreadability of the product on the skin and prevent the separation of active ingredients, thereby extending the shelf-life and improving the tactile experience of the cosmetic.
Safety, Biodegradability, and Environmental Impact
One of the most significant advantages of using plant-based fibers is their absolute biodegradability. As a natural plant fiber product, it returns to the environment without leaving toxic residues, aligning with the global shift toward green chemistry and sustainable manufacturing.
Safety profiles are equally impressive. It is recognized as safe for human consumption and application; because it is not absorbed by the human body, it is naturally excreted through the digestive tract, making it a low-risk choice for both medical and food-grade applications.
The transition toward enzymatic production further enhances this eco-friendly profile. By reducing the use of harsh acids and minimizing waste, the industry is moving toward a circular economy where high-performance materials do not come at the cost of environmental health.
Technical Specifications and Quality Standards
To ensure consistent performance, high-grade eucalyptus cellulose products must adhere to strict parameters. This includes a pH range of 5.0 to 7.5 and extremely low limits for heavy metals (≤ 10 ppm) and arsenic salts (≤ 2 ppm), ensuring that the material does not contaminate the final product.
Particle size is another critical factor, with specifications often split between grades like PH-101 (50μm) and PH-102 (100μm). These variations allow manufacturers to choose the exact grade that fits their specific machinery and desired tablet hardness.
Compliance with the Chinese Pharmacopoeia (2020 edition) serves as a benchmark for quality, ensuring that every batch meets rigorous tests for water-dissolved matter, chloride levels, and microbial counts to guarantee sterility and purity.
Technical Specification Analysis for MCC Derivatives
|
Specification Item
|
PH-101 Grade
|
PH-102 Grade
|
Standard Limit
|
| Average Particle Size |
50 μm |
100 μm |
Customizable |
| Moisture Content |
≤ 0.5% |
≤ 3.5% |
Low Humidity |
| Water Solubility |
≤ 0.2% |
≤ 0.2% |
Insoluble |
| Heavy Metals |
≤ 10 ppm |
≤ 10 ppm |
≤ 10 ppm |
| Burning Residue |
≤ 0.1% |
≤ 0.1% |
≤ 0.1% |
| Conductivity |
≤ 75 us/cm |
≤ 75 us/cm |
≤ 75 us/cm |
FAQS
It is primarily due to its high compressibility and porous structure. This allows it to bind active ingredients into hard, stable tablets while simultaneously acting as a disintegrant that allows the tablet to break down quickly once ingested, improving drug bioavailability.
Yes, microcrystalline cellulose derived from plant sources is considered safe for food use. It acts as an anti-caking agent and stabilizer, and because it is not absorbed by the human body, it is safely excreted through the digestive tract.
The main difference lies in the average particle size and moisture content. PH-101 has a smaller particle size (50μm) and lower moisture (≤0.5%), while PH-102 is larger (100μm) with slightly higher moisture (≤3.5%), allowing manufacturers to choose based on their specific formulation needs.
Acid hydrolysis removes the amorphous regions of the cellulose molecule, leaving behind a crystalline structure. This process significantly enhances the material's compressibility and stability, turning raw fiber into a functional industrial excipient.
Absolutely. It is used to increase the viscosity of lotions and creams, improving the texture and spreadability. It also helps stabilize formulas, preventing the separation of oils and water-based ingredients over time.
Modern production is increasingly sustainable. While acid hydrolysis is traditional, the shift toward enzymatic hydrolysis reduces chemical waste. Furthermore, the end product is completely biodegradable, making it an eco-friendly alternative to synthetic polymers.
Conclusion
In summary, the transformation of eucalyptus cellulose into Microcrystalline Cellulose provides the global manufacturing sector with a high-performance, safe, and sustainable material. Its unique ability to function as a binder, filler, and stabilizer across the pharmaceutical, food, and cosmetic industries underscores its versatility and technical importance. By maintaining strict adherence to quality standards like the Chinese Pharmacopoeia, the industry ensures that these plant-based derivatives deliver consistent results in complex formulations.
Looking forward, the adoption of green chemistry through enzymatic hydrolysis will further solidify the role of cellulose in a sustainable future. For companies seeking to enhance product stability and environmental credentials, integrating high-purity cellulose derivatives is a strategic necessity. To explore our full range of high-grade cellulose products, visit our website: www.tangzhihpmc.com